If you’ve ever ordered cored wire from a supplier—whether you’re a steel mill technician, a foundry foreman, or a metallurgy lab manager—you know that a shipment that arrives damaged or improperly stored before use can derail your entire production schedule. Over the past 12 years, I’ve run a cored wire supply company out of the Midwest, and I’ve seen just how many avoidable mistakes happen when transporting this specialized product. I’ve had customers call me at 2 a.m. screaming because their last shipment of ferro-silicon cored wire arrived rusted, unspooled, or bent so badly it wouldn’t feed into their wire feeder. That’s why I want to pull back the curtain on what we teach every one of our logistics teams, and what we walk through with every new customer, to make sure cored wire gets to you safely, every single time. Let’s break this down step by step, no fancy jargon, just the lessons I’ve learned loading thousands of pallets and troubleshooting dozens of shipment emergencies. Cored Wire
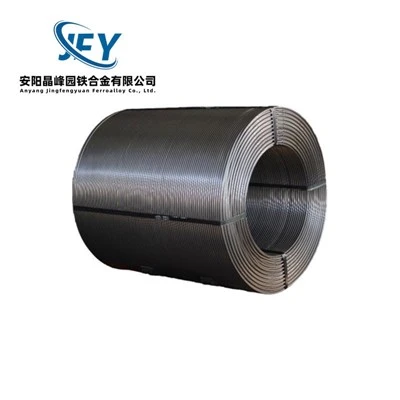
First, let’s get one thing straight: cored wire isn’t your average spool of wire. It’s a hollow steel tube filled with fine powdered alloys—ferro-silicon, calcium silicide, rare earth metals, all the additives that turn raw molten metal into high-quality steel, cast iron, or ductile iron. The tube is paper-sealed at both ends to keep moisture out, and when it’s bent, dropped, or exposed to extreme temperature swings, two bad things happen. First, the seal breaks, letting moisture seep into the powder. That sounds small, but that moisture will react with the molten metal in your furnace, causing hydrogen porosity—tiny bubbles in the final product that can make a steel beam fail a stress test or a casting crack unexpectedly. Second, the steel tube can kink or crack during transport. A kink might not be visible to the naked eye, but when you feed that wire at 10 to 30 meters per minute into your ladle or feeder, the kink will lock up, break the feeder tip, or dump half a load of additives into the wrong spot. I once had a customer in Detroit reject an entire 20-ton shipment of ferro-magnesium cored wire because a single driver tried to stack our pallets on top of a shipment of heavy machinery parts. The bottom pallet’s plastic wrap split, and the top pallet’s edge crushed the first two layers of wire spools. Each spool was 500 kilograms, so the crumpled wire was useless—they had to stop their ductile iron line for 12 hours to reorder, costing them over $80,000 in downtime. That’s the kind of story that makes me obsessed with transport protocols, and it’s the first lesson I’ll give you: packaging and loading aren’t just logistics details—they’re quality control.
Let’s start with packaging, because that’s your first line of defense before the wire even leaves our warehouse. Not all cored wire packaging is created equal, and I’ve seen suppliers cut corners here to save a few cents per pallet. At our company, every spool of cored wire we produce gets wrapped in two layers: first, a food-grade polyethylene plastic liner that’s heat-sealed shut to create an airtight barrier. We make sure to squeeze every last bit of air out of the liner before sealing, because trapped air holds moisture, especially in humid climates like the Gulf Coast or the Southeast. Then, we wrap the entire spool in a heavy-duty, 100-micron stretch film, applied in at least six overlapping layers, to hold the liner tight and add a second layer of physical protection. For smaller spools (under 1,000 kilograms), we stack them on wooden pallets that are heat-treated and marked for international shipping—no pallets that are chipped, splintered, or have protruding nails, because those can puncture the plastic liner during loading. For larger, heavy spools (over 1,500 kilograms), we skip the pallets entirely and cradle them in custom-cut, double-thick foam inserts that line the base of our wooden crates. The foam absorbs 90% of the impact from bumps and sudden stops, which is huge for long-haul trucking or rail transport. I’ll admit, a few years ago we tried switching to thinner stretch film to cut costs, and within two months we had three customers complaining about moisture damage. We switched back to the heavy film, and those complaints dropped to zero. That’s not rocket science—it’s paying attention to the little details that make a difference.
Next, it’s all about how you load and secure those pallets or crates onto the truck, train car, or shipping container. I’ve seen drivers load cored wire next to sharp metal parts, heavy construction equipment, or even empty pallets that can shift during transit. That’s a recipe for disaster. The first rule of loading cored wire is to never stack heavy, pointy, or shifting cargo on top of it. Cored wire spools are round and heavy—you don’t want a 2-ton forklift part sliding off a pallet and crushing a stack of spools. At our warehouse, we reserve the front third of every dry van truck for cored wire shipments, because that spot is less likely to shift when the driver brakes suddenly or hits a pothole. We also secure every row of pallets with two heavy-duty ratchet straps, placed 1 meter apart along the length of the truck, not just across the top. I learned this the hard way five years ago: a driver on a cross-country run hit a patch of ice in Ohio, and a single strap broke when he slammed on his brakes. The pallet of spools rolled forward, crashing into the cab’s bulkhead, and half the spools were bent beyond use. Since then, we never use less than two straps per pallet, and we check every single strap before it leaves the loading dock. If it has a fray, a broken hook, or any sign of wear, we throw it away—no exceptions. For international shipments going in ocean containers, we add wooden dunnage blocks between every two rows of pallets to prevent shifting during rough sea transit. We also fill any gaps between pallets with foam insulation, not cardboard, because cardboard compresses and leaves space for the pallets to move. A container that sways across the Atlantic is no place for a loose cored wire shipment.
Climate control is another big one, especially if you’re transporting cored wire long-distance or during extreme weather. Most people don’t think about temperature and humidity when shipping metal, but I can’t stress this enough. Cored wire should never be exposed to temperatures above 50°C or below -10°C, and humidity levels under 60% are ideal. Why? High humidity makes the steel tube rust, and rust causes two problems: it can clog your wire feeder, and when you feed rusted wire into molten metal, the rust oxidizes and pulls oxygen out of the metal, which weakens its strength. Extreme cold makes the plastic liner brittle, so it can crack during loading or transit, letting moisture in. Extreme heat, on the other hand, can soften the adhesive that seals the paper inside the tube, and the paper can tear, spilling the powder. A few years ago, we shipped a batch of rare earth cored wire to a foundry in Texas during July—our driver refused to put it in a non-air-conditioned truck, and he was right. The temperature inside the truck hit 58°C during the day, and when the foundry unloaded it, the adhesive on the paper seals had melted, and three spools had spilled half their powder. If we had put that in a non-air-conditioned truck, we would have lost the entire batch. Now, for any shipment going to areas with temperatures over 40°C or under 0°C, we require our logistics team to use either a temperature-controlled truck or insulated shipping containers. We also include a small, silica-gel moisture absorber inside every plastic liner—we put two for shipments going to tropical climates, and one for temperate areas. That little extra step has saved us from so many moisture-related complaints.
Then there’s the matter of handling, especially when it comes to unloading. I’ve seen warehouse workers drop a spool of cored wire 2 meters to the ground, or use a forklift to hook the edge of a crate instead of the pallet’s forks. That’s a surefire way to damage the wire. Every one of our spools is marked with big, bold “THIS SIDE UP” and “FRAGILE” labels, and we make sure our customers and their drivers know to read those. We also provide free, downloadable guides on our website for unloading cored wire: use a forklift with forks that slide fully under the pallet, never try to lift a spool by its outer edge (it can warp the core), and never drop it, even from a small height. I once had a customer in Chicago call me panicking because their unloading driver dropped a 1,000-kilogram spool from 1 meter onto the concrete floor. The spool looked fine, but when they unspooled 5 meters of wire, it had a hidden kink that broke their feeder. They had to replace a $2,000 feeder tip, and their production line was down for 3 hours waiting for a replacement. That’s $20,000 worth of downtime over a $5 mistake. We now include a free unload checklist with every shipment, and we spend 10 minutes walking through the correct unloading steps with every first-time customer, just to make sure that doesn’t happen to them.
I also want to touch on what to look for when you receive a cored wire shipment, because even with all the proper transport steps, accidents can still happen. Before you sign for a delivery, do a quick visual check of the pallets or crates. Are there any punctures in the plastic wrap? Any dents or cracks in the wooden crates? Any spools that are protruding at odd angles? If you see any of these, note it on the delivery receipt before the driver leaves, and take photos. That way, if there’s hidden damage, you have proof to file a claim with the carrier. We always tell our customers to do this—we’d rather take a little time to inspect the shipment than argue about a damaged load later. Once you sign for it, the clock starts, so to speak, on any damage claims, and it’s much harder to get the carrier to take responsibility. I once had a customer in Canada who signed for a shipment without checking, and two weeks later they found that the plastic liner had a small puncture from a nail in the pallet. They tried to claim against the carrier, but since they didn’t note it on the delivery receipt, the carrier refused to pay. We ended up replacing half the shipment for free, just to keep a good customer, but it taught us that inspection is non-negotiable.
Over the years, I’ve had dozens of customers tell me that they used to have a lot of problems with cored wire transport until they started working with us. One foundry in Ohio used to order wire from a supplier that cut corners on packaging and loading, and they were getting 15% of their shipments damaged every month. Since they switched to us two years ago, that number has dropped to less than 1%. The secret isn’t some fancy technology or new packaging—it’s paying attention to every step, from the second the wire is wound onto the spool to the second it’s unloaded at the customer’s facility. Every part of that process matters, because even one damaged spool can cost a production line thousands of dollars.
At the end of the day, transporting cored wire safely isn’t just about getting a product from Point A to Point B. It’s about making sure your production runs on time, your final metal products meet quality standards, and you don’t have to deal with unexpected downtime or wasted materials. If you’re tired of dealing with damaged, improperly shipped cored wire, or if you’re ready to switch to a supplier that prioritizes safety as much as you do, I’d encourage you to reach out to our team for a consultation. We can walk you through our transport protocols, answer any questions you have, and even provide case studies from other customers who’ve seen the difference in reliable cored wire shipments. Don’t let transport mistakes derail your next project—let’s work together to make sure your cored wire arrives safe, every single time.
Cored Wire References
- American Foundry Society. (2019). Cored Wire Handling and Transport Guidelines for Ferrous Metal Production. AFS Press.
- International Society of Automation. (2021). Standard Practices for Packaging and Transport of Metallurgical Additives in Cored Wire Form. ISA Publications.
- Transportation Safety Administration. (2020). Guidelines for Shipping Bulk Industrial Metallurgical Products. TSA Logistics Safety Division.
- Steel Industry Suppliers Association. (2018). Best Practices for Cored Wire Packaging and Transit to Global Markets. SISA Technical Bulletin.
Anyang Jingfengyuan Ferroalloy Co., Ltd.
As one of the most professional cored wire manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy bulk cored wire in stock here and get quotation from our factory. We also accept customized orders.
Address: Longquan Town Industrial Park, Long’an District, Anyang City, Henan Province
E-mail: Jingfengyuan@jfyferroalloys.com
WebSite: https://www.jfy-ferroalloy.com/
