Hey folks, let’s cut to the chase—if you’re here googling “rotary lime kiln operating cost,” odds are you’re not just daydreaming about lime production. You’re either a plant manager staring at next quarter’s budget, a maintenance lead crunching numbers to justify an upgrade, or maybe a new operations guy who just inherited a kiln that’s been eating cash like it’s going out of style. I’ve sold rotary lime kilns for over 12 years, so I’ve seen every stupid, avoidable cost that creeps in and every hidden saving that makes the math make sense. Let’s break this down like we’re chatting over a coffee (no stuffy spreadsheets—promise). Rotary lime kiln

First, let’s get one thing straight: there’s no one-size-fits-all number here. A 100 tpd kiln for a small lime processor? Total operating costs are way different than a 500 tpd unit that runs around the clock for a steel mill. But we can split these costs into buckets so you can map ’em to your setup, not some generic industry fluff. The biggest chunk by far? Energy. That’s not “electricity” like a toaster, either—rotary lime kilns run on fuel to heat limestone to 900–1000°C (1650–1830°F) to turn it into quicklime. I’ve seen guys guess fuel costs, then get shocked when their actual bill is 20% higher because they forgot about heat loss through the kiln shell.
Wait, let’s define quicklime production basics real quick. Every ton of finished quicklime requires roughly 1.1 tons of limestone, right? That’s your feedstock cost, the second biggest line item, but let’s start with energy because it’s the one that trips up new operators. Modern rotary lime kilns use either natural gas, coal, or fuel oil—most now lean on natural gas because it’s cheaper and cleaner than it was 10 years ago, but I still have customers in places where coal is way more affordable. Let’s run a quick example: for a 300 tpd kiln, the energy requirement is around 7.5–8.5 GJ per ton of quicklime. If natural gas is $10 per GJ, that’s $75–$85 per ton, but that’s only if the kiln is running efficiently. If your shell is leaking heat (old seals, cracked insulation), or your burners are misaligned, that number jumps 15–25%. I had a customer a couple years back with a 250 tpd kiln that was wasting 30% of its heat through the shell—we swapped the seals and added high-density insulation, and their fuel costs dropped $12,000 a month. That’s not chump change, that’s a new millwright’s salary, or a parts budget buffer.
Next big bucket: labor. Running a rotary kiln isn’t pushing buttons and walking away. You need a shift crew—usually 3–4 people per 8-hour shift—plus a lead operator, a maintenance tech on call, and sometimes a helper. This varies so much by location: if you’re in a place with low labor costs, that’s $30–$40 per hour per crew, but if you’re in Europe or North America, that’s $50–$70 an hour, plus benefits. Wait, but here’s a hidden cost most folks miss: overtime. Kilns almost never shut down for small repairs unless it’s an emergency, because firing one back up takes 2–3 days and uses a ton of fuel. So if a bearing goes out on a Saturday, you’re paying double time for the tech who has to fix it while the kiln’s idling, not shut down. I’ve seen that add $5,000–$10,000 a month in extra labor if maintenance is sloppy.
Then there’s maintenance and parts. Rotary kilns are heavy, rotating machines—wear is non-negotiable. The big ticket items: refractory brick (lines the kiln, has to be replaced every 1–3 years, depending on how hard you run it), kiln tires and rollers (those grind against each other, so they need resurfacing or replacing every 5–10 years), seals (we’ve developed self-adjusting seals that cut seal wear by 40%, by the way), and bearings. Wait, but maintenance costs aren’t just parts—they’re downtime. If your kiln is down for 24 hours, that’s 24 hours of no production, plus fuel to keep it warm while you fix it, plus lost revenue from not shipping quicklime. A buddy who runs a cement plant once told me an unplanned kiln outage cost him $150,000 in one day. That’s way more than the cost of a good preventive maintenance schedule. Oh, and for my new customers: don’t cheap out on refractory. I’ve seen guys buy cheap brick to save a few bucks, only to have it crack in 6 months, leading to a full kiln reline that costs 3x more than the “cheap” brick savings.
Wait, what about smaller, easier-to-miss costs? Let’s call them the “nickel-and-dime” stuff that adds up. Water: some kilns use water for cooling the bearings or the baghouse (the pollution control system). Air for the combustion burners. Chemicals for emissions control—if you’re in a region with strict EPA rules, you might have to inject lime or ammonia to scrub SO2 or NOx. And electricity! Most people forget that even when the kiln’s heating, it’s turning 50+ meters of steel cylinder, so the motor that drives the rotation uses a ton of power. For that same 300 tpd kiln, electricity is $10–$15 per ton of quicklime. Add that to the buckets I mentioned earlier, and let’s do a total rough number: for a mid-sized (200–300 tpd) modern kiln running 24/7, total operating costs are roughly $120–$180 per ton of quicklime. Wait, but let’s compare that to an old kiln we might’ve sold 10 years ago—those same kilns were $180–$250 per ton, because they were way less efficient. That’s the difference between a well-engineered kiln and a clunky old unit.
Now, let’s talk about the biggest variable that makes this number swing: efficiency. I can’t stress this enough. Modern rotary lime kilns have features that slash operating costs, but only if you actually use them. Let’s list the efficiency wins: preheaters! Adding a 2-stage or 3-stage preheater means you’re using the exhaust heat from the kiln to warm up the limestone before it even enters the hot zone. That cuts fuel use by 20–30%—I’ve had customers go from $90 per ton fuel costs to $60 just by adding a preheater. Then there’s variable frequency drives (VFDs) for the kiln motor. Old kilns run at a fixed speed, even when you’re producing less than max, wasting electricity. VFDs let you adjust the speed to match production, cutting electricity use by another 10–15%. And those self-adjusting seals I mentioned? They stop air from leaking into the kiln, which messes up combustion and adds fuel waste. That’s another 5% in fuel savings.
Wait, what about if you’re running a smaller kiln, like 50 tpd for a local construction company? The operating costs per ton go up, right? Because you’re not getting the economies of scale. For that tiny kiln, total costs are more like $180–$250 per ton, because fuel, labor, and parts don’t scale down evenly. I had a customer who runs a 75 tpd kiln in rural Texas—he was paying $220 per ton for years, then we tweaked his burner, added a preheater, and he got it down to $165 per ton. That’s $55 per ton saved, and he’s producing 200 tons a day—so $11,000 extra a month, just from some small upgrades.
Now, let’s talk about the myths I hear all the time. Myth #1: “Buying a cheaper kiln means lower operating costs.” No way. I sold a super cheap kiln to a guy in Ohio a few years back, and it broke down every 3 months. The operating costs (parts, downtime, overtime) ended up being 2x higher than if he’d bought a more reliable, efficient unit from us. Myth #2: “Fuel costs are the only big one.” Like I said earlier, labor and maintenance make up 30–40% of total operating costs, so skimping on maintenance will kill you way faster than a 10% fuel price hike. Myth #3: “All rotary lime kilns are the same.” I can promise you that’s not true. The design—whether it’s a parallel flow, cross flow, or counter flow kiln—matters. Counter flow is the most efficient, because exhaust air flows opposite to the limestone, so you recover way more heat. That’s why most modern kilns are counter flow.
Wait, should we talk about hidden savings when production is high? If you’re running the kiln at 90–100% capacity, your per-ton costs drop a lot, because fixed costs (labor, parts) are spread over more tons. If you only run it at 50% capacity, those fixed costs are on half the production, so per-ton costs jump 20–25%. That’s why we always tell customers to size their kiln to their actual demand, not what they think they might need in 5 years. Oversizing is a recipe for wasted money.
Let’s wrap this up with a real-world example from a customer I worked with last year. He had a 400 tpd rotary lime kiln that was built in 2008, running on natural gas. His total operating costs were $195 per ton. We did an audit, found that his seals were worn, his refractory was starting to fail in sections, his VFD was broken so he was running at fixed speed, and his burner was outdated. We replaced the seals with our self-adjusting ones, did a full refractory reline (using high-alumina brick that lasts longer), fixed the VFD, and swapped the burner for a low-NOx, high-efficiency unit. After three months, his costs dropped to $142 per ton. That’s $53 per ton saved, which for 400 tons a day is $63,600 a month. He paid us $280,000 for all the upgrades, so he paid that back in about 4 months. That’s not a fluke—that’s what good maintenance and smart upgrades do.
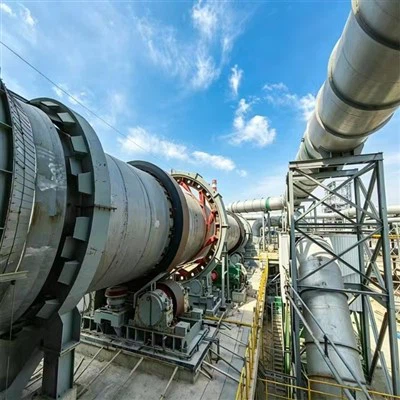
So, if you’re sitting here trying to figure out what your rotary lime kiln’s operating cost will be, the first step is to stop guessing and start with an audit. We do free kiln audits, by the way—we’ll come out to your site, check your fuel use, production rates, maintenance logs, everything, and give you a real, tailored number, not some industry average. If you’ve got an old kiln that’s eating cash, or you’re looking to buy a new one and want to know what it’ll actually cost to run, hit us up for a chat. We don’t do pushy sales stuff—we just help guys get their numbers right, because that’s how we’ve stayed in business this long.
PCC Plant References
- Rotary Lime Kiln: Energy Efficiency and Operating Cost Analysis, International Journal of Process Industries, 2021
- Lime Production Handbook, National Lime Association, 2022
- Industrial Rotary Kiln Maintenance Best Practices, Society for Maintenance & Reliability Professionals, 2020
- Fuel Selection and Cost Optimization for Lime Kilns, Energy Efficiency and Management Journal, 2019
- Small-Scale Lime Processing: Cost Structures and Scaling Effects, Journal of Sustainable Industrial Chemistry, 2023
Handan Metallurgical Engineering & Research Co., Ltd.
Handan Metallurgical Engineering & Research Co., Ltd. is well-known as one of the leading rotary lime kiln manufacturers and suppliers in China. We warmly welcome you to buy high quality rotary lime kiln made in China here from our factory. Good service and competitive price are available.
Address: Cheng’an County, Handan City, Hebei Province, China
E-mail: hanhaizhao@dzmer.com
WebSite: https://www.dzmer.com/
